Direct wholesale B2B solutions with complete quality control, private labeling, and global logistics support.

An authoritative analysis on low-molecular-weight plant oligopeptides, enzymatic hydrolysis optimization, and functional performance in cosmetic & nutraceutical matrices.
Hydrolyzed Rice Protein (INCI: Hydrolyzed Rice Protein) is a naturally derived cosmetic and food-grade peptide ingredient obtained by treating non-GMO rice (Oryza sativa) protein isolates with targeted endo- and exo-peptidases. Unlike native rice proteins, which exhibit poor water solubility and high molecular weight (>50 kDa), our controlled enzymatic cleavage process reduces the average molecular mass to between 500 Da and 2,000 Da.
This micro-molecular profile contains an exceptionally rich spectrum of essential amino acids, including Glutamic Acid, Arginine, Aspartic Acid, and Lysine. At the cellular level, these bioactive oligopeptides interact seamlessly with keratinous substrates (skin stratum corneum and hair cuticle fibers), providing superior moisture retention, anti-irritation properties, and structural film formation without sticky residues.
| Parameter / Attribute | Standard Commercial Grade | Shaanxi Bieyouth Premium Grade | Formulation Benefit |
|---|---|---|---|
| Average Molecular Weight | 3,000 – 5,000 Da | < 1,000 Da High-Penetration Fraction | Deeper stratum corneum absorption & cuticular repair |
| Color & Clarity (5% Sol.) | Yellowish Brown, Slight Haze | Pale Yellow to Off-White, Completely Clear | Ideal for high-end clear serums & transparent beverages |
| Odor Profile | Distinct Grain/Fermentation Odor | Ultra-Low Odor (Deodorized Enzymatically) | Requires minimal fragrance masking in personal care |
| Allergenicity | Variable Plant Traces | Hypoallergenic Certified & Gluten-Free | Safe for sensitive skin formulations & baby care products |
Our eco-friendly, zero-waste bio-refinery process guarantees strict lot-to-lot consistency and maximum biological activity.
Sourcing non-GMO, pesticide-free rice protein isolates with initial purity > 80% from audited agricultural partners.
Application of food-grade endopeptidase and exopeptidase at controlled temperature (50–55°C) and pH to cleave peptide bonds.
Multi-stage ceramic nanofiltration to segregate desired molecular weight distribution (<2000 Da) and remove insoluble ash.
Brief High-Temperature Short-Time (HTST) thermal treatment to permanently deactivate enzyme catalysts while preserving bioactive peptide structures.
Low-temperature spray drying under clean-room conditions to yield a highly soluble, uniform powder with low moisture content (<5%).
How leading global formulators in North America, Western Europe, Asia-Pacific, and Latin America utilize Hydrolyzed Rice Protein across diverse product categories.
In clean-beauty markets across the US and Europe, Hydrolyzed Rice Protein serves as a vegan replacement for animal keratin and silk peptides. It binds to damaged hair cuticles, expanding shaft diameter by up to 14.5%. Widely incorporated into volume-boosting shampoos, leave-in conditioners, and scalp barrier repair serums.
K-Beauty and J-Beauty formulators utilize micro-hydrolyzed rice peptides to stimulate collagen synthesis and inhibit matrix metalloproteinases (MMPs). Its natural abundance of proline and glycine supports skin elastic fiber integrity, reducing fine lines and boosting hydration in facial sheet masks and barrier creams.
As a non-dairy, hypoallergenic protein source, Hydrolyzed Rice Protein offers rapid gastric emptying and instantaneous amino acid absorption. Ideal for post-workout recovery powders, ready-to-drink (RTD) plant beverages, and allergy-safe meal replacement bars targeting fitness enthusiasts.
Leveraging Shaanxi Bieyouth Biotech's robust industrial integration, direct factory pricing, and scale economies to secure customer margins worldwide.
Located in Shaanxi, China—a hub of botanical extract innovation and agricultural logistics—our raw material procurement utilizes long-term agricultural contracts. This insulates our global partners from market price volatility and ensures consistent, non-GMO raw rice protein reserves year-round.
Operating dual standardized GMP workshops equipped with multi-ton continuous extractors and automated spray dryers allows us to lower unit manufacturing costs dramatically. We pass these savings directly to brand owners, contract manufacturers, and distributors through "Discount" factory-direct wholesale pricing.
Our dedicated foreign trade export division provides seamless shipping logistics (FOB, CIF, DDP, DDU) with full documentation compliance—including Certificate of Analysis (COA), MSDS, Allergen Statements, ISO, Kosher, and Halal certificates.
Staying compliant in international markets with robust regulatory validation and sustainability parameters.
Hydrolyzed Rice Protein is fully listed on the European Commission CosIng database. Complies with strict European limits for heavy metal traces, residual solvents, and microbial safety. Perfectly matches the strict EU microplastics and non-animal testing directives.
Our facilities are US FDA registered, ensuring smooth clearance under the Modernization of Cosmetics Regulation Act (MoCRA). Ingredients qualify for GRAS (Generally Recognized As Safe) status when utilized in food and dietary supplement matrices.
Derived via enzymatic biotransformation with zero hazardous chemical effluents. Biodegradable, non-ecotoxic to marine ecosystems, and fits 100% vegan, cruelty-free, and Halal/Kosher formulation requirements.
Integrating world-class extraction technology, rigorous quality systems, and customized OEM/ODM services since 2018.
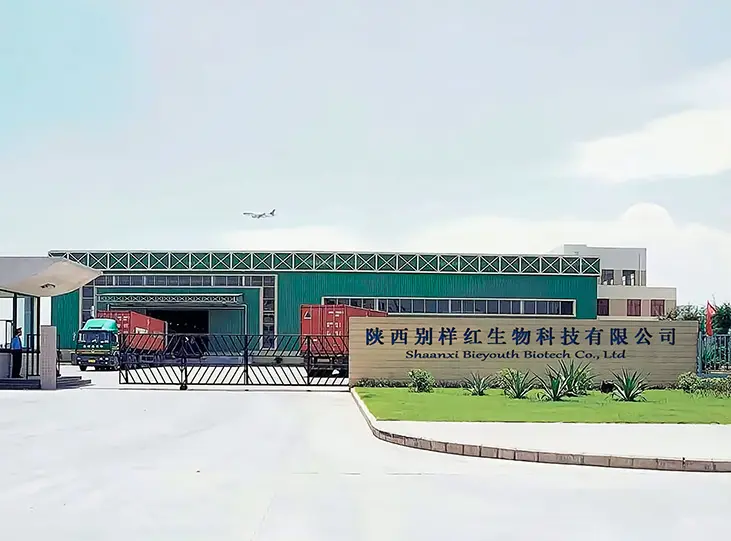
Shaanxi Bieyouth Biotech Co., Ltd. was established in 2018, with years of experience in foreign trade import and export. It is a large-scale gold supplier integrating production and sales. We mainly specialize in plant and animal extracts, food additives, cosmetic raw materials, and pharmaceutical raw materials.
Our production facilities are GMP certified, with two standardized production workshops and advanced extraction equipment. Our high-purity ingredients are exported to the United States, the United Kingdom, Canada, Russia, Australia, and other parts of the world.
Scientific Research Breakthroughs
Quality Control System
Capacity Leap
Annual Production Capability
Participated in Shanghai International Cosmetics, Personal & Home Care Raw Materials Exhibition (PCHi).
Obtained official FDA certification from the US Food and Drug Administration.
Expanded global trade footprint and built the Institute of Biology for cosmetic raw material research.
Awarded prestigious titles of "Integrity Enterprise" and "Quality Assured Enterprise".
Investigating targeted bio-active compounds in energy replenishment formulations.
June 12, 2026 • Natural rosmarinic acid applications.
June 12, 2026 • Safety evaluation & lipid oxidation control.
June 12, 2026 • Cellular ATP bioenergetics & cardiovascular health.
Shaanxi Bieyouth Biotech Co., Ltd. offers comprehensive OEM and ODM services. Our streamlined process includes:
In-depth alignment on target specs, quality benchmarks, and volume requirements.
Customized hydrolysis engineering, liquid or powder dosage matching.
Rapid prototyping and COA analytical report dispatch for client sign-off.
Strict batch inspection and global direct shipping under private label.
Rated Great with over 1,223 verified B2B reviews on Trustpilot worldwide.

Key technical, quality, and commercial inquiries answered by our senior technical directors.
Explore our complete catalog of factory-direct bio-pharmaceutical and cosmetic solutions.
 Bieyouth